English
 Português
 Español


Conclusion: The HQ600-S-7P LT offers reliable CNC punching and cutting for panels and transformers in Argentina. Processes copper and aluminum with CNC precision aligned with IRAM/IEC practices and Mercosur projects. Designed for workshops in Buenos Aires, Córdoba, Rosario and Santa Fe that seek to manufacture at home.
Test condition — punching:copper T2 10×100 mm at 25 °C; 500 cycles at nominal load. Concentricity Ø13 mm ≤0.15 mm; average burr <0.1 mm (typical hand saw 0.3–0.5 mm).
Test condition — folding/cutting:same material; 90° folding with standard matrix. Mean angular deviation ≤0.5°; cutting parallelism ≤0.2mm/100mm (manual shear ±0.8mm).
Productivity Baseline:board type part (6 holes + 2 cuts + 1 bending) ≈ 45–60 s in CNC versus 3–5 min in equivalent manual process.
CNC Copper Busbar Punching Machine
Model: HQ600-SP
Main Function
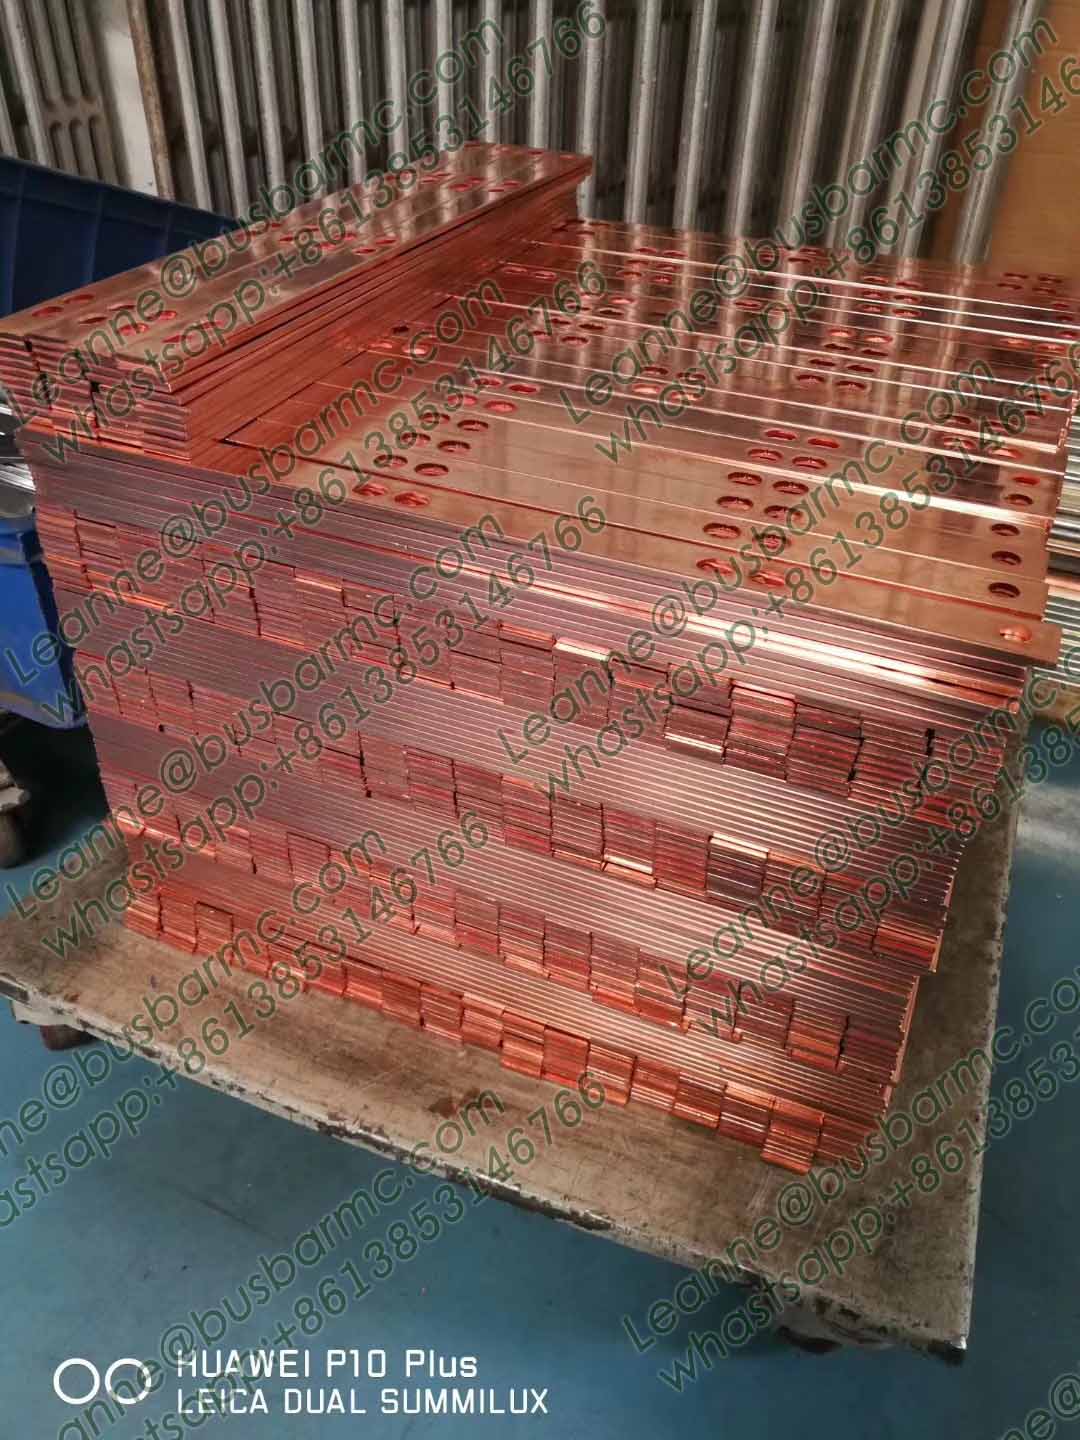
Cut, punch, chamfer, emboss (all kinds of round, square, special holes and slot type) the copper, aluminum busbar etc.



Main Features
This machine specializes in processing copper and aluminum busbars for high and low voltage systems, offering high efficiency, low energy consumption, precision, ease of use, and a modern design.
This machine features unique processing principles, a patented hydraulic cylinder system, and a daily capacity of several tons, making it the top choice for busbar processing.
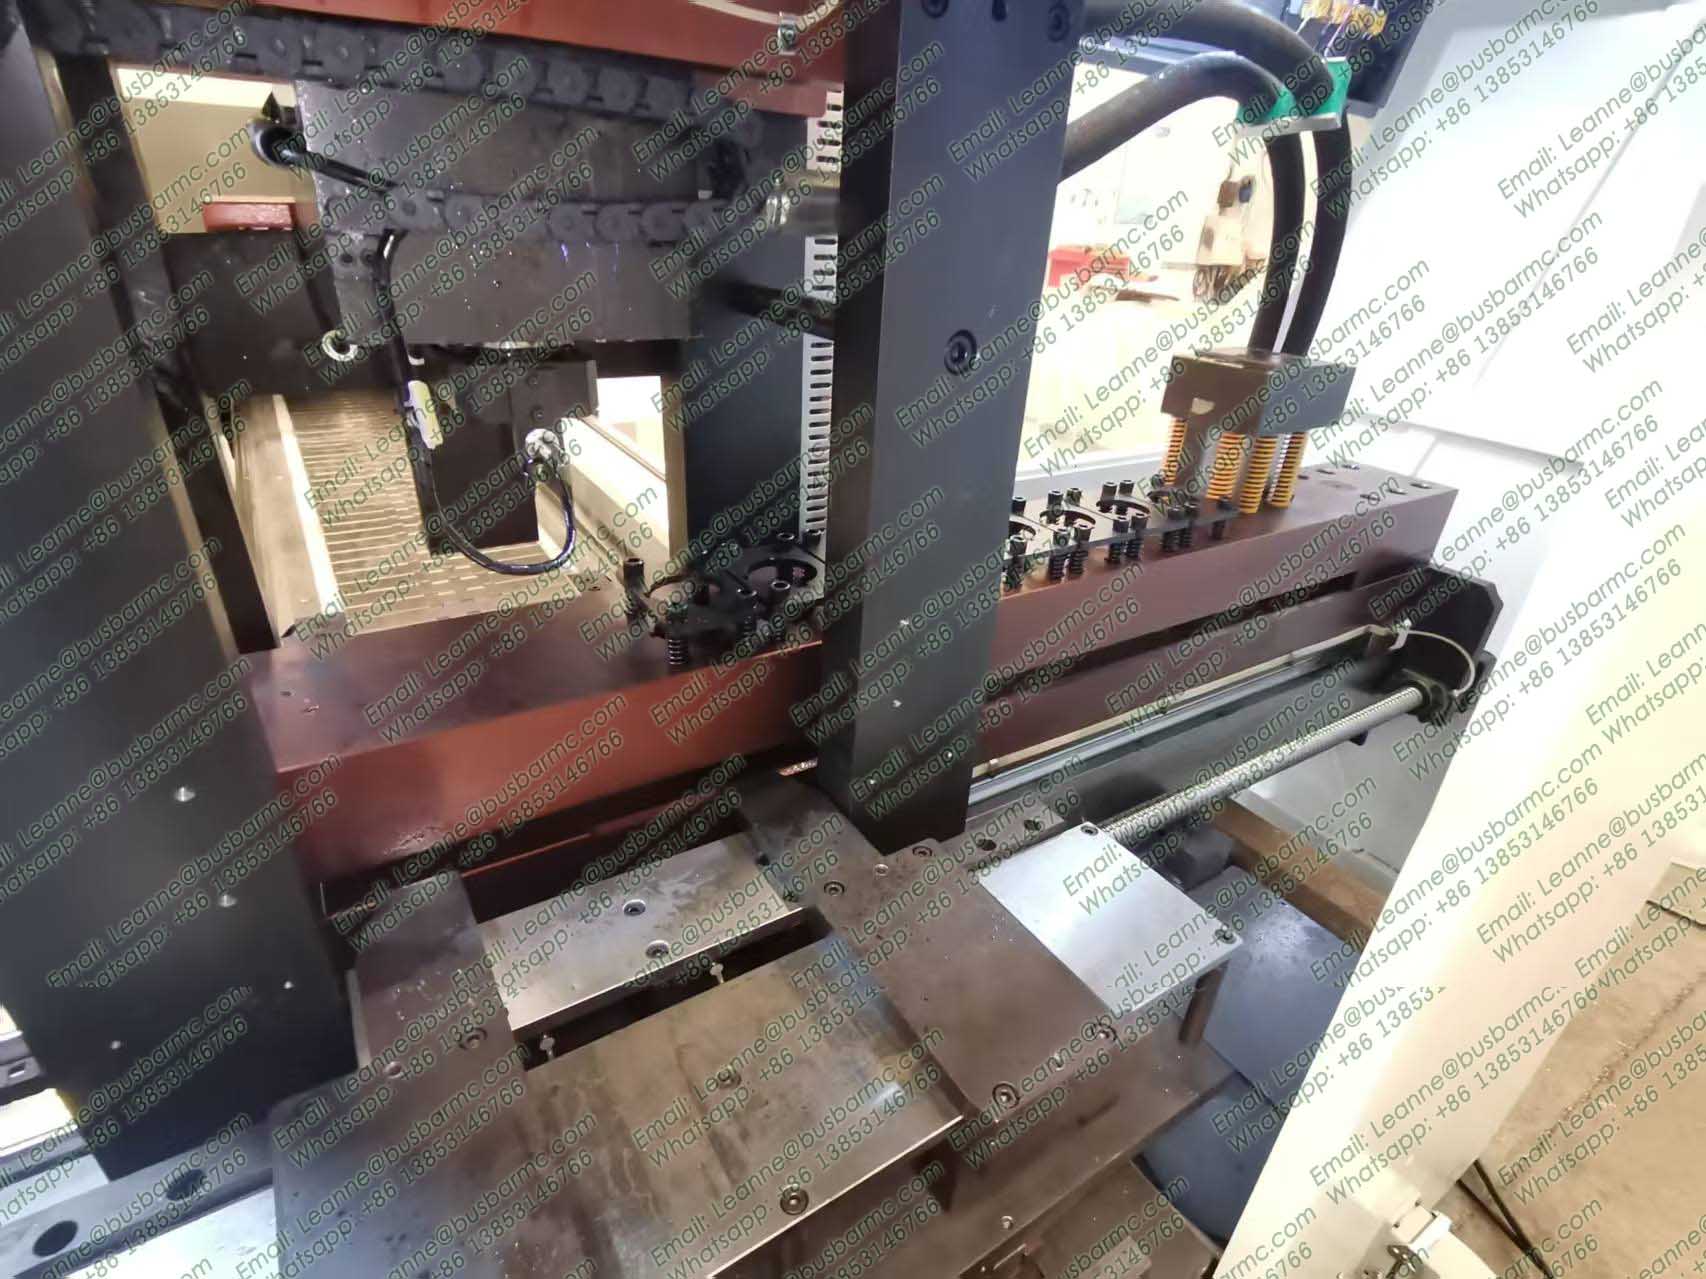
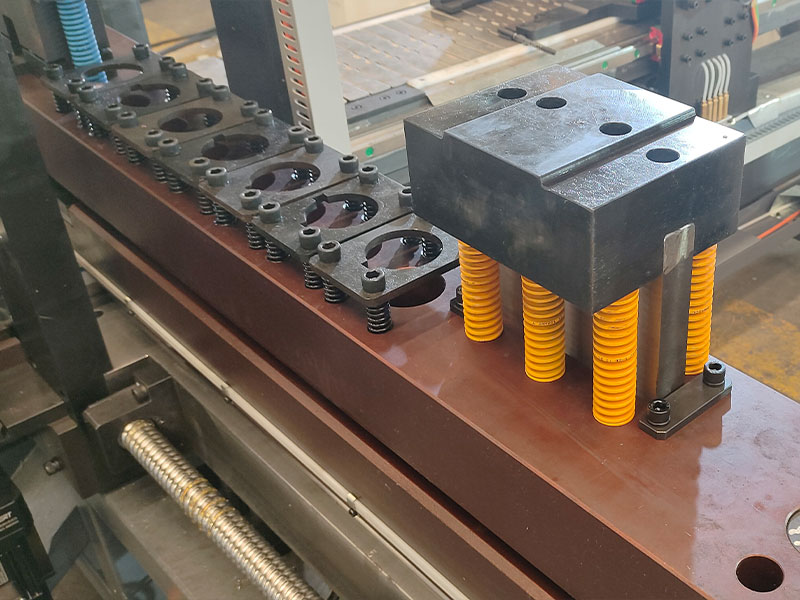
It allows single clamping for long busbars, automating punching and shearing without manual intervention through automatic clamp switching. Optional 7/8-punch and 1-shear inline die sets; embossing available.
Cutting dies is a single pole type hedge Scissor, no waste after shearing.
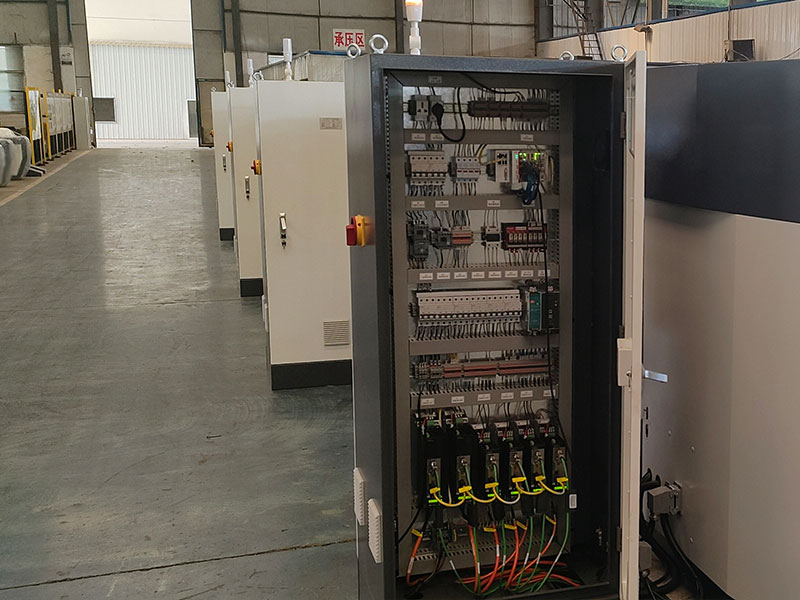
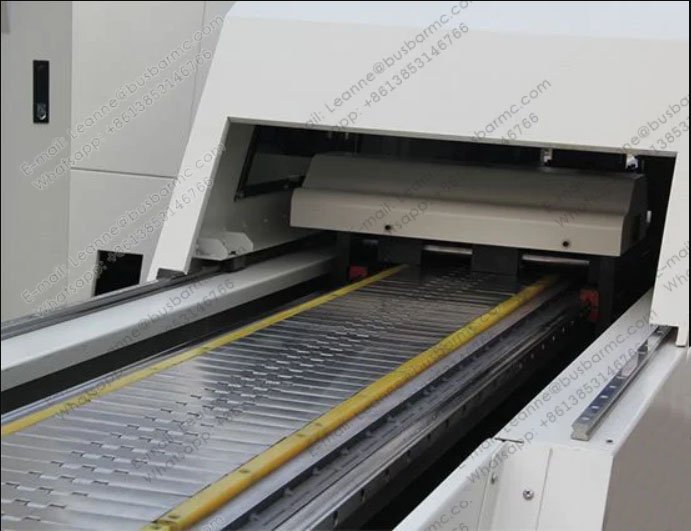
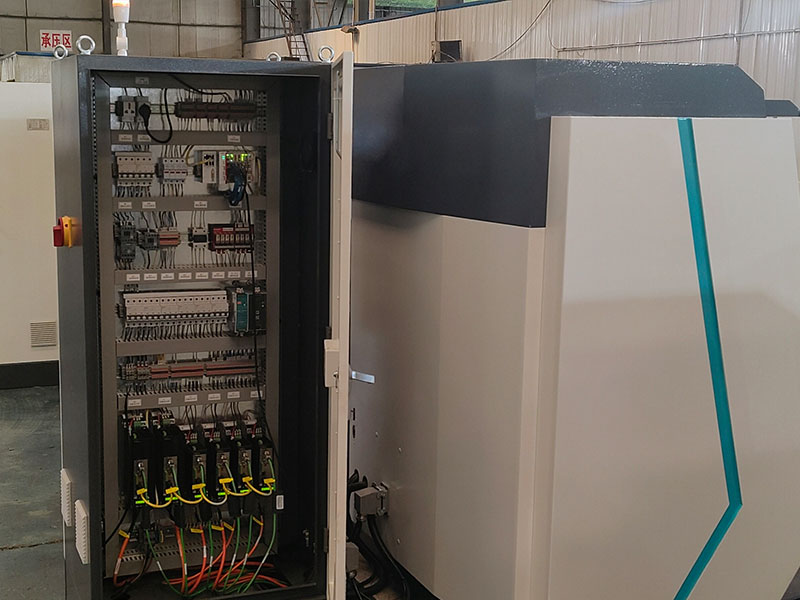
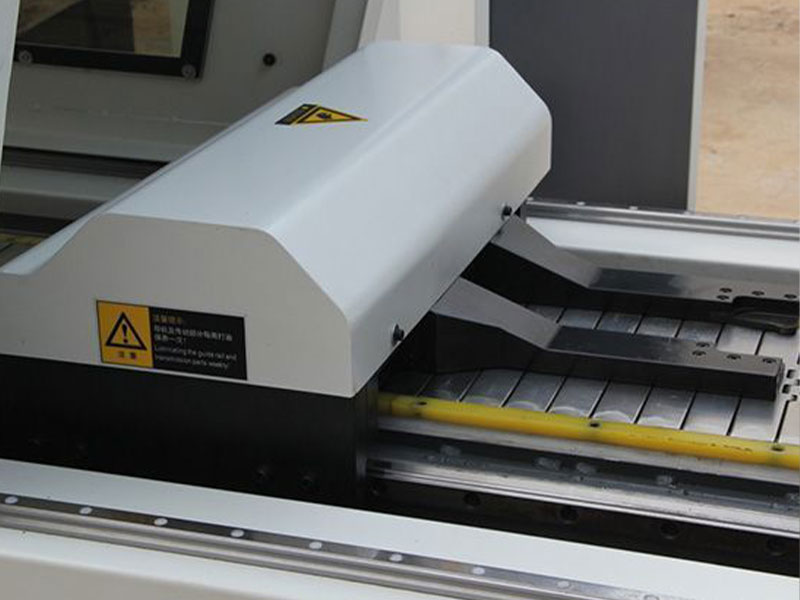
The machine comprises a feeding table, mould base, conveying system, servo control unit, and assistant design system, delivering stable and reliable performance.
Featuring a user-friendly interface and the self-developed BMC busbar processing design system, it provides real-time monitoring of program operations.
The mould base, made of ductile iron, offers excellent wear resistance, ensuring long-term Concentricity of punching molds.
Technical Parameters
| Parameter | Model | HQ400-S-7P/8P | HQ600-S-7P/8P |
|---|---|---|---|
| Nominal Pressure | 400KN | 600KN | |
| Maximum Processing Size | 12×160mm | 15×200mm | |
| Punching Range | Φ4.3-25mm | Φ4.3-35mm | |
| Maximum Number of Molds | 8punch 1shear | 8punch 1shear 7punch +1emboss |
|
| X-Axis Max Travel | 2000mm | 2000mm | |
| X-Axis Positioning Speed | 60m/min | 75m/min | |
| Y-Axis Max Travel | 860mm | 960mm | |
| Y-Axis Positioning Speed | 35m/min | 35m/min | |
| Z-Axis Max Travel | 200mm | 310mm | |
| Z-Axis Positioning Speed | 35m/min | 35m/min | |
| Punching Accuracy | ±0.2mm | ±0.2mm | |
| Positioning Accuracy | 0.10/500mm | 0.10/500mm | |
| Punching Speed | 100 times/min | 120-150 times/min | |
| Number of Control Axes | 6 Axis | 6 Axis | |
| Machine Dimensions (L×W×H) | 10500×2750×1700mm | 10500×2900×1800mm |
Optional Accessories
| Part Name | Option 1 | Option 2 |
|---|---|---|
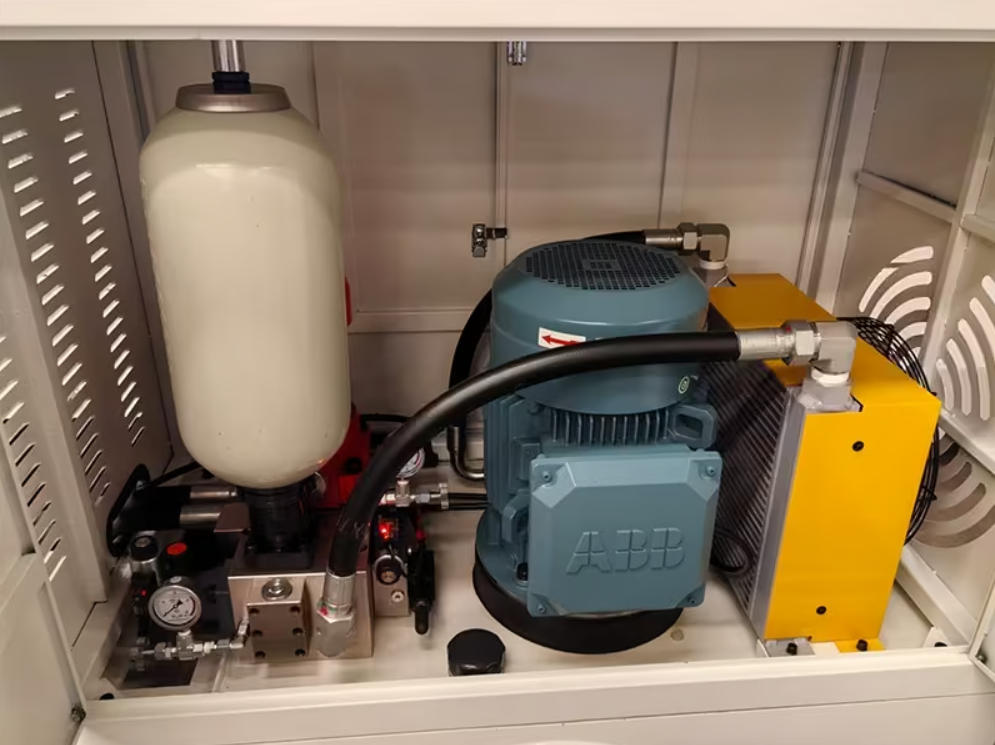
| Main Motor | July | ABB |
| Hydraulic Pump | Taiwan Hydromax | American Albert |
| Solenoid Valve | Taiwan Litand | German Rexroth |
| Guides/Screws | HIWIN / TBI/PMI | HIWIN / TBI/PMI |
| Servo System | Exton | German Rexroth |
| Industrial Computer | Taiwan PanelMaster (Touch Screen) | Beijing Qiyang |
Random Accessories
8 sets of punching dies, 1 shear blade, 1 set of maintenance tools, and manuals with certificates included.